How to install threaded inserts in wood
Threaded inserts for wood turn a tired hole in a chair rail, table legs, a bed frame or a plywood cabinet into a permanent, reusable metal mounting point. The installation takes a drill, a hex wrench and five minutes if the pilot hole is right.
Pick the thread, then the length
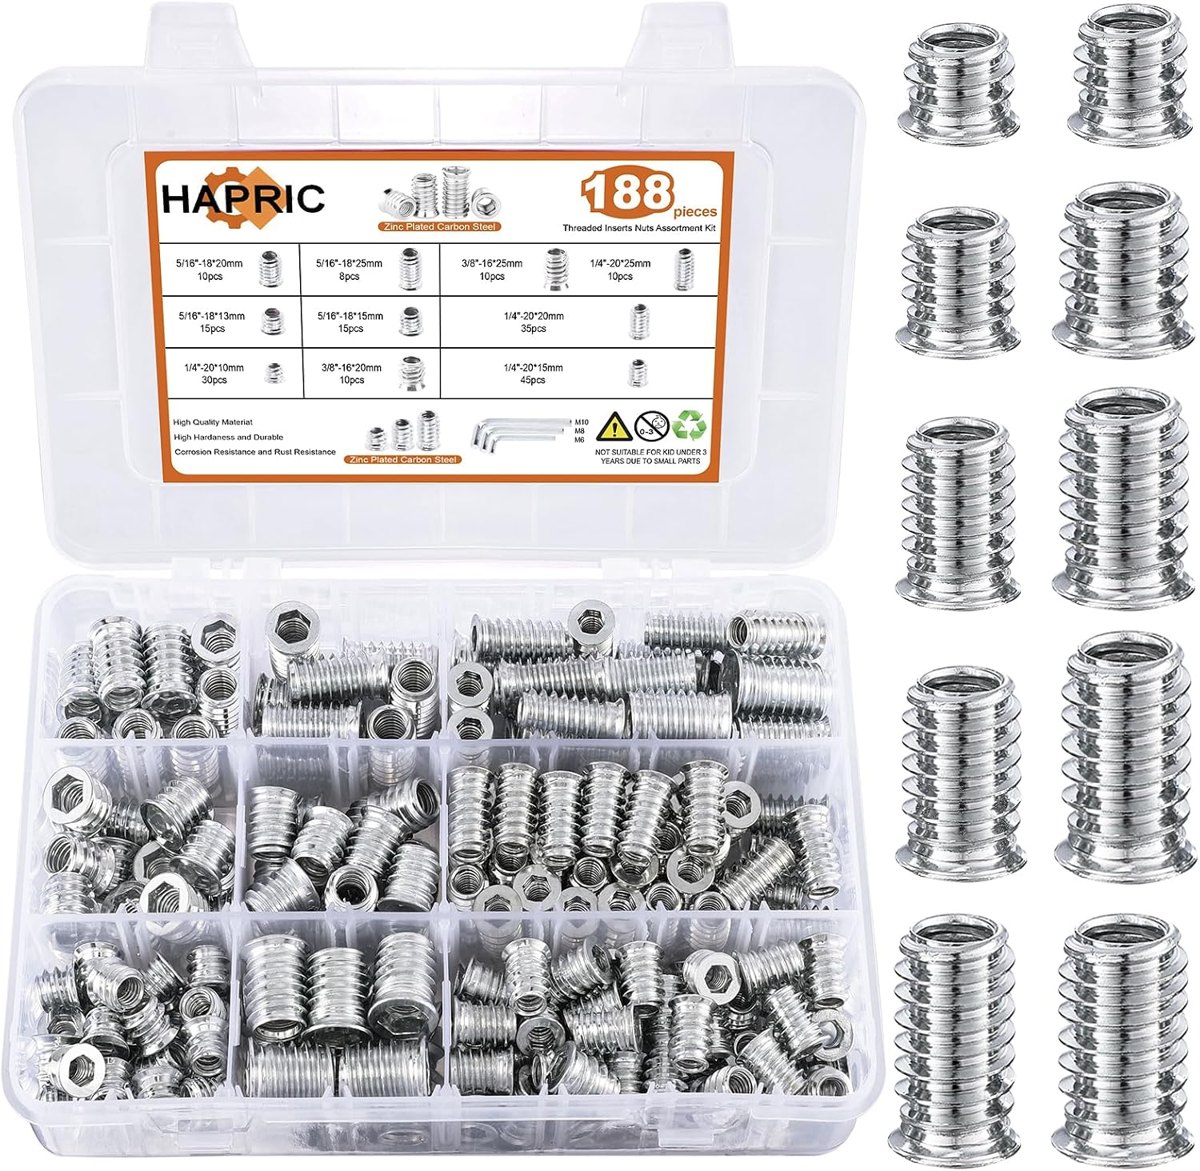
1/4-20 is the furniture standard and fits most bolts that come with knock-down pieces. 5/16-18 suits table legs and workbench tops; 3/8-16 is for benches, jigs and anything that carries real load or vibration. Choose an insert length that leaves at least 3 mm of wood behind it in a blind hole, and a bolt that stops short of the far face. The material of the board sets the rest: softwood, plywood and MDF take the standard pilot, hardwood takes a slightly larger one.
Drill the pilot hole to the core, not the knurl
The external knurl is meant to cut into the wood, so the hole matches the core: roughly 9.5 mm for 1/4-20, 11 mm for 5/16-18 and 12.5 mm for 3/8-16 in pine, plywood and MDF. In oak, maple or other hardwood go about 0.5 mm larger. Drill square to the surface; a drill press or a simple block jig keeps the insert from leaning. No tap is needed: the insert cuts its own seat.
Drive it with the hex wrench
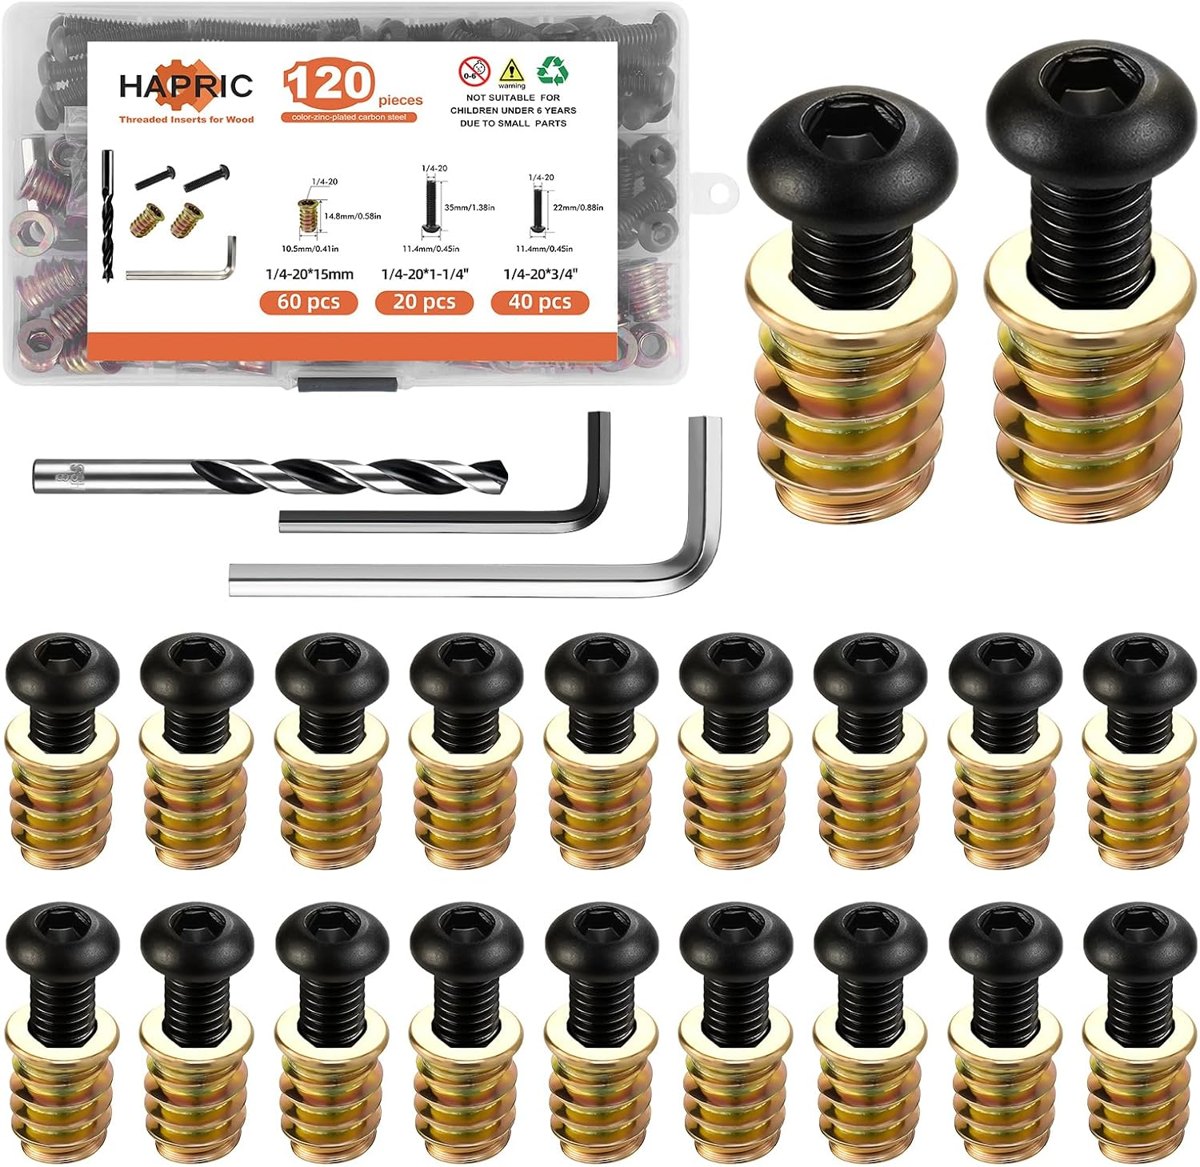
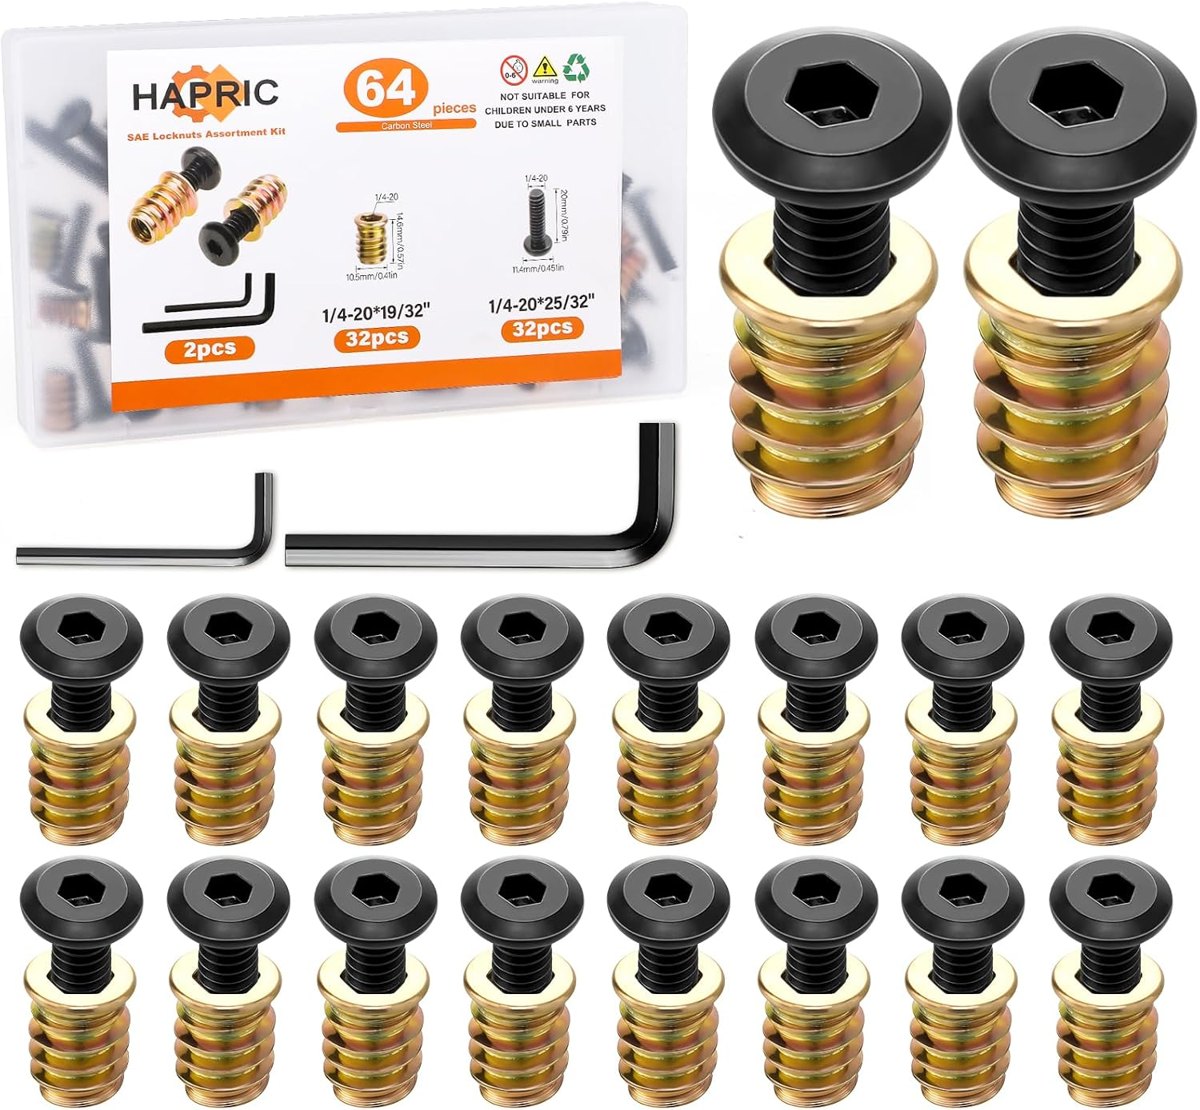
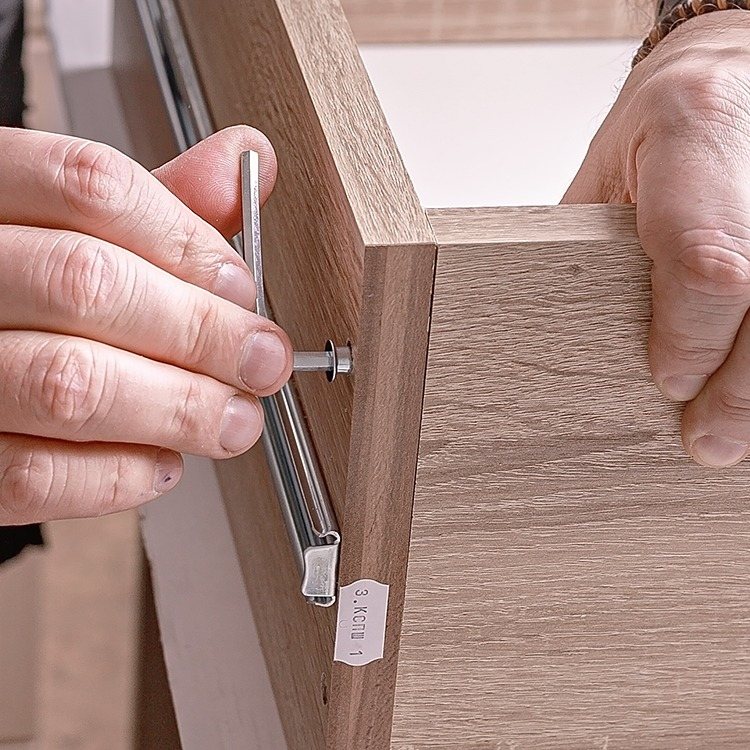
Put the hex wrench into the insert's internal thread, hold it vertical and turn slowly until the insert sits flush or just below the surface. If it starts to lean, back it out and restart. In soft particle board a drop of wood glue or epoxy in the hole before driving adds grip and seals the fibres; in hardwood a touch of wax on the knurl eases the cut and protects the board from splitting.
When the old hole is already stripped
Drill the stripped hole out to the insert's pilot size and drive the insert in; the knurl grips fresh wood around the damage and the assembly can be bolted and unbolted again without wear. Where the panel is thin, use the shorter 10 or 13 mm inserts from our 191-piece kit and a bolt sized to match.
For plastic, use heat instead
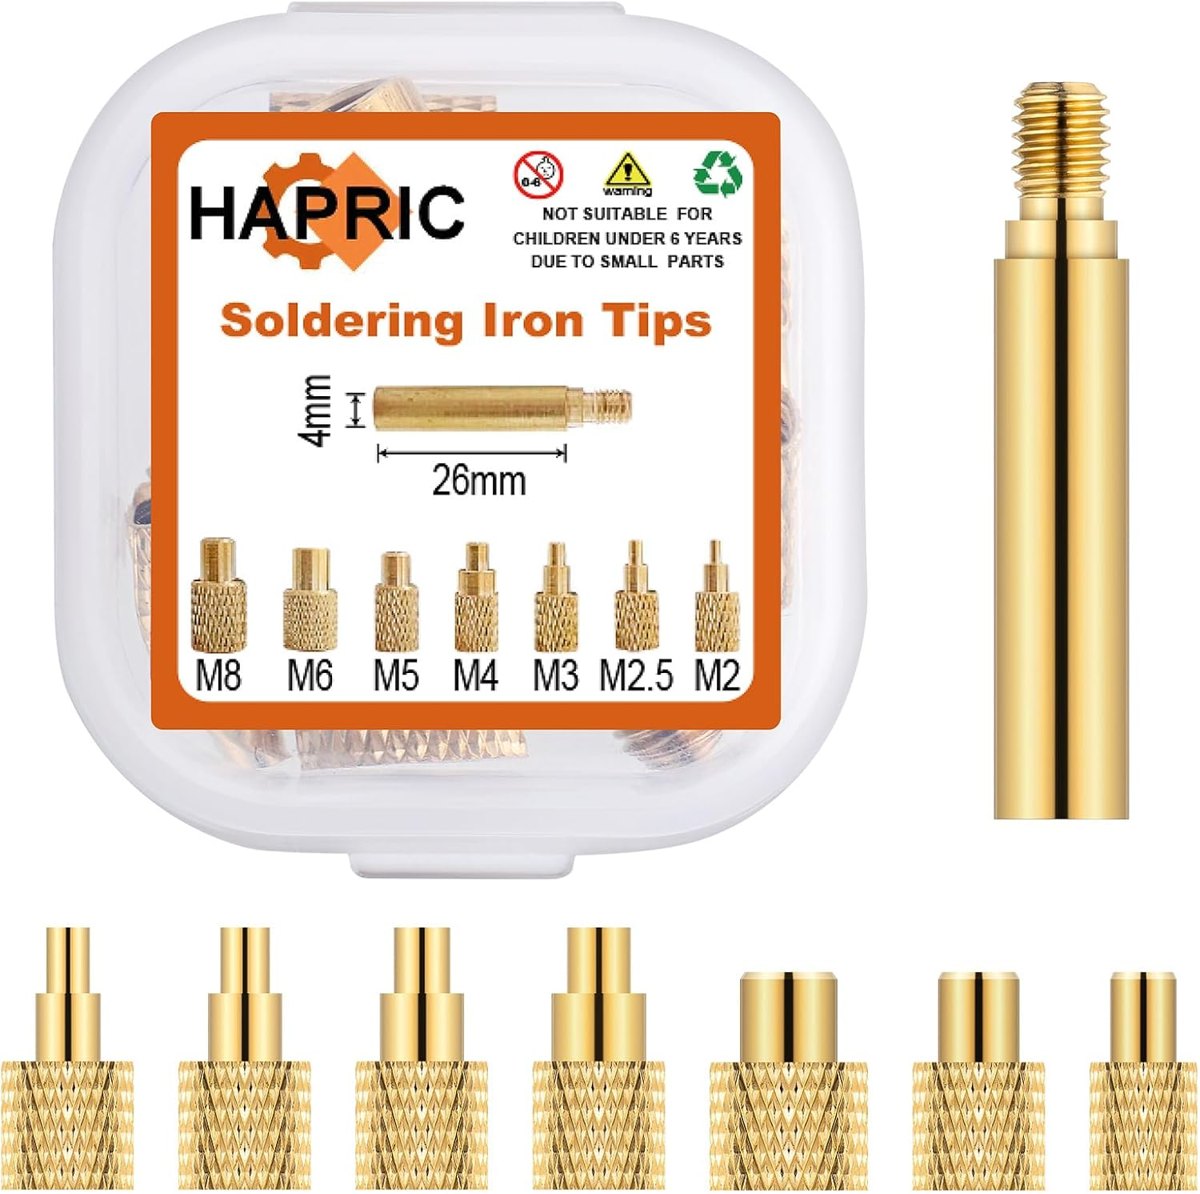
Threaded inserts for plastic are pressed in hot. Our brass heat-set tips screw onto a soldering iron and match M2 to M8 inserts; set the iron around 200 degrees Celsius for PLA and PETG, rest the insert on the boss and let the weight of the iron sink it straight.